类别
最新博客
标签
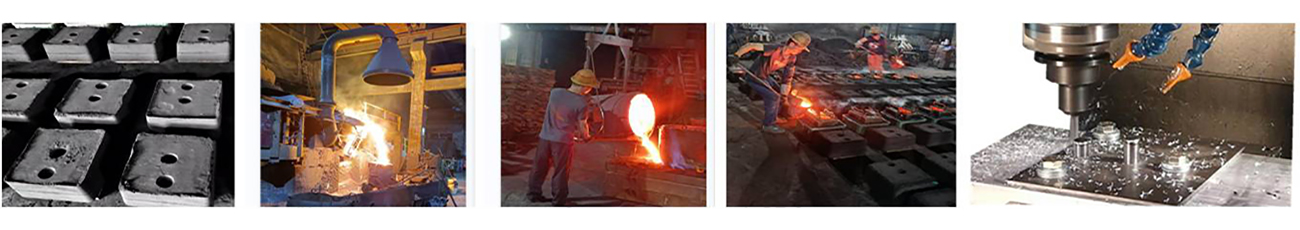
Dimensional accuracy is a key quality requirement for sand cast iron parts, especially when components must fit into larger mechanical assemblies. For pump housings, valve bodies, agricultural machinery, construction equipment, and industrial machine bases, even small dimensional deviations can increase machining costs, delay assembly, or affect equipment performance.
Sand casting is widely used to manufacture complex iron components because it offers flexible design options, relatively low tooling costs, and the ability to produce large, heavy parts. However, dimensional variation can occur at several stages, from pattern manufacturing and mold preparation to metal solidification, cooling, and final machining.
Understanding these factors helps manufacturers improve consistency and enables buyers to specify realistic tolerances for custom iron castings.
The pattern determines the basic shape and dimensions of a sand casting. If its dimensions are incorrect, the resulting mold cavity may reproduce the same errors.
Common problems include pattern wear, machining inaccuracies, incorrect shrinkage allowances, and insufficient machining stock. Wooden patterns may also change dimensions due to moisture and temperature, while metal patterns generally provide better dimensional stability during repeated production.
To improve accuracy, manufacturers should verify critical pattern dimensions, inspect tooling regularly, and establish suitable allowances based on the iron grade, casting geometry, and production process. Correct datum locations and machining allowances should also be agreed upon before production begins.
For high-volume production, well-maintained metal patterns can improve repeatability. For prototypes and low-volume custom sand cast iron parts, careful pattern inspection remains essential.
Molding sand directly affects the stability of the mold cavity. Grain size, moisture content, binder concentration, permeability, and compaction all influence mold strength and dimensional consistency.
Excessive moisture or inconsistent compaction can weaken the mold, allowing its walls to move or deform under molten iron. Uneven mold hardness may also cause local expansion, erosion, or dimensional differences between castings.
| Mold-related factor | Possible dimensional problem | Recommended control |
|---|---|---|
| Inconsistent sand moisture | Variable mold strength | Monitor moisture and sand properties |
| Uneven compaction | Local deformation or expansion | Standardize molding parameters |
| Low mold strength | Erosion or mold-wall movement | Optimize sand and binder quality |
| Poor mold alignment | Parting-line mismatch | Check alignment and clamping |
| Worn equipment | Repeated dimensional errors | Inspect and maintain tooling |
These controls are particularly important for large sand casting parts, where even minor mold movement can create significant dimensional deviations.
Metal shrinkage is one of the main causes of dimensional variation in cast iron components. As molten iron cools, it undergoes thermal contraction. The final dimensional change depends on chemical composition, graphite formation, casting geometry, mold conditions, and cooling history.
Grey iron and ductile iron behave differently during solidification because graphite formation and expansion influence their volume changes. Consequently, the same pattern shrinkage allowance should not automatically be applied to every casting.
Wall thickness also matters. Thick sections cool more slowly than thin sections, potentially causing uneven contraction, residual stress, and distortion. Foundries can reduce these problems by selecting suitable shrinkage allowances, optimizing section geometry, and using appropriate gating and riser systems.
Casting simulation can help identify hot spots and predict solidification behavior in complex industrial components before production begins.
It is also important to distinguish dimensional shrinkage from shrinkage porosity. The former changes the size or shape of a casting, while the latter creates internal or surface voids because molten metal cannot adequately feed areas that contract during solidification.
Pouring temperature influences molten iron fluidity, mold heating, and solidification behavior. If the temperature is too low, the metal may fail to fill thin sections completely. Excessively high temperatures can increase thermal exposure and contribute to mold erosion or other process-related problems.
Cooling rate is equally important. When different sections of a casting cool at different speeds, uneven contraction can cause bending, twisting, or dimensional distortion.
There is no universal pouring temperature for all sand cast iron parts. The appropriate range depends on the iron grade, section thickness, casting weight, gating design, and foundry process.
Manufacturers should establish process-specific temperature limits, maintain consistent pouring practices, and validate cooling procedures for critical components. Controlled cooling is especially valuable for large industrial castings with complex geometries.
Pump housings, valve bodies, engine components, and pipe fittings often contain internal passages that require sand cores. If a core shifts during mold assembly or pouring, the casting may have incorrect internal dimensions or uneven wall thickness.
Poor core support, insufficient core strength, and inaccurate core prints can all contribute to this problem. Similarly, misalignment between the upper and lower mold sections, known as the cope and drag, can create a mismatch along the parting line.
Manufacturers should inspect core dimensions, verify core seating, use suitable locating features, and check mold alignment before pouring. For castings requiring extensive machining, accurate core positioning is particularly important because uneven wall thickness can leave insufficient material around critical bores or mounting features.
Residual stress develops when different sections of a casting contract unevenly during cooling. Complex shapes, abrupt wall-thickness changes, asymmetrical designs, and restrictive mold conditions can increase the risk of distortion.
A casting may meet its initial dimensional requirements but change shape during subsequent heat treatment, handling, or machining. Removing material from one side can release internal stress and cause the remaining component to move.
This is a common concern for large machine bases, heavy equipment iron castings, and precision-machined pump housings.
Balanced geometry, controlled cooling, suitable stress-relief treatment where specified, and a planned machining sequence can help reduce distortion. Critical dimensions should be inspected at the appropriate production stage rather than relying solely on measurements taken immediately after shakeout.
Even a well-designed casting can show dimensional variation when production parameters are not maintained consistently. Changes in sand preparation, pattern condition, pouring practice, operator technique, and inspection methods may create differences between batches.
Measurement conditions also matter. Large castings should be measured at a stable temperature, using calibrated equipment and clearly defined reference points.
Depending on the component's geometry and tolerance requirements, inspection methods may include calipers, micrometers, height gauges, dedicated fixtures, coordinate measuring machines (CMMs), portable measuring arms, or laser scanning.
First-article inspection and documented in-process checks help identify deviations before they become recurring production problems.
The most effective strategy is to control variation throughout the manufacturing process rather than relying entirely on final inspection.
| Production stage | Recommended action | Expected benefit |
|---|---|---|
| Design review | Confirm tolerances, datums, and machining stock | Fewer design-related errors |
| Pattern production | Verify dimensions and shrinkage allowances | Better mold-cavity accuracy |
| Mold preparation | Control sand properties and compaction | Improved mold stability |
| Core assembly | Check location, support, and alignment | Reduced wall-thickness variation |
| Pouring and cooling | Standardize process parameters | More consistent solidification |
| Heat treatment and machining | Control treatment and machining sequence | Reduced distortion |
| Final inspection | Use calibrated equipment and documented checks | Reliable dimensional verification |
Tolerance requirements should reflect the function of each feature. A noncritical exterior surface generally does not need the same precision as a bearing seat, sealing face, mounting hole, or machined bore.
As a general reference, larger conventional sand castings may require dimensional allowances measured in several millimeters, depending on their size and geometry. Selected features can achieve tighter dimensions through improved process control and machining, but these capabilities must be confirmed with the foundry rather than assumed.
ISO 8062-3 provides a framework for dimensional and geometrical tolerances and machining allowances for castings. The appropriate tolerance grade should be agreed upon according to the drawing, casting process, component dimensions, and supplier capabilities.
When choosing a custom casting manufacturer, industrial buyers should evaluate process control and inspection capability alongside unit price. A reliable supplier should explain how it manages pattern accuracy, mold stability, shrinkage, cooling, and machining.
Before placing an order, confirm:
Clear engineering drawings and agreed inspection criteria help reduce misunderstandings, rework, and unnecessary production costs.
For OEMs and industrial equipment manufacturers, the goal is not to apply the tightest possible tolerance to every surface. It is to achieve the accuracy required for reliable assembly and operation at a commercially reasonable cost.
By controlling pattern design, molding conditions, metal shrinkage, cooling behavior, core positioning, and inspection procedures, manufacturers can improve the consistency of sand cast iron parts and reduce dimensional problems in demanding industrial applications.


 IPv6 网络支持