类别
最新博客
标签
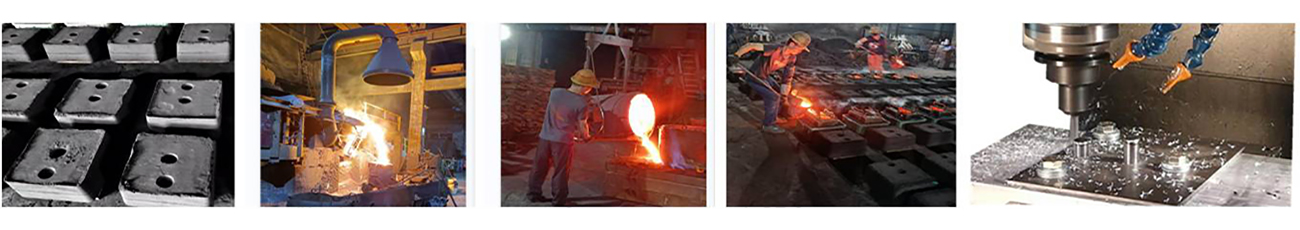
Machining costs can account for a significant portion of the total manufacturing cost of cast iron components. Although sand casting is a cost-effective way to produce complex industrial parts, excessive machining, unnecessarily tight tolerances, and poor casting geometry can quickly increase production expenses.
For OEMs and industrial equipment manufacturers, reducing machining costs starts during the design stage, long before a component reaches the machine shop. Decisions about material selection, wall thickness, machining allowance, and feature placement all influence production time, tool life, and finished-part quality.
Whether you manufacture custom cast iron parts, gray iron castings, ductile iron components, pump housings, valve bodies, or heavy machinery components, a well-planned design can reduce machining requirements without compromising strength, dimensional accuracy, or service life.
One of the simplest ways to reduce machining costs is to avoid applying tight dimensional tolerances to every feature.
Tight tolerances often require additional machining passes, more precise fixtures, frequent measurements, and stricter process control. However, many external surfaces and non-functional features do not need the same accuracy as bearing seats or sealing interfaces.
For example, an industrial pump housing may require precise dimensions for bearing bores, shaft openings, and gasket surfaces. Its external reinforcing ribs, however, may function perfectly well with standard as-cast tolerances.
| Feature | Recommended approach | Cost-saving benefit |
|---|---|---|
| Bearing bores | Specify tolerances according to shaft or bearing fit | Avoids unnecessary precision |
| Gasket surfaces | Define flatness and surface finish requirements | Maintains sealing performance |
| Mounting holes | Set position tolerances based on assembly needs | Reduces inspection time |
| External profiles | Use suitable as-cast tolerances | Eliminates unnecessary machining |
| Non-functional ribs | Retain as-cast surfaces where practical | Reduces machining operations |
The appropriate tolerance depends on the casting process, component size, material, and functional requirements. For example, a bearing seat may need finish boring to achieve its specified fit, while a non-contact surface may not require machining at all.
The goal is to control critical dimensions carefully without paying for precision that does not improve product performance.
Every machined surface adds cutting time, tool consumption, setup requirements, and potentially inspection costs. Designing suitable features to remain in the as-cast condition can therefore lower the cost of custom iron castings.
Sand casting offers considerable flexibility for producing complex geometries, including ribs, bosses, mounting structures, and reinforcing sections. If these features can be formed reliably in the mold and do not require precise contact surfaces, machining may be unnecessary.
Consider a large industrial machine base with multiple reinforcing ribs. Machining every rib surface would add little functional value if those surfaces do not affect alignment, assembly, or load transfer.
By contrast, bearing supports, sliding interfaces, gasket seats, and precision mounting faces generally require controlled machining.
A practical design rule is to machine only the surfaces that have a clearly defined functional requirement. This is particularly valuable for large sand casting parts, where extensive surface machining can require large machine tools, specialized fixtures, and additional material handling.
Casting geometry affects both casting quality and the amount of machining required afterward. Abrupt section changes, poorly designed junctions, and unnecessarily thick walls can contribute to uneven solidification, shrinkage defects, and dimensional distortion.
These problems may require additional machining allowance or lead to rejected components.
When designing cast iron parts, engineers should aim for reasonably uniform wall thickness wherever practical. Gradual transitions and appropriate corner radii can help improve metal flow and reduce stress concentrations.
Several design practices are worth considering:
For example, a ductile iron pump housing with an excessively thick central section may cool differently from its thinner surrounding walls. The resulting distortion can complicate bore alignment and increase machining difficulty.
However, reducing wall thickness indiscriminately is not a solution. Minimum wall thickness must account for the iron grade, casting dimensions, filling conditions, pressure requirements, and structural loads. The foundry should review these factors before the design is finalized.
Machining allowance is the extra material left on a casting so that machining can produce the required final dimensions and surface finish.
Excessive allowance increases cutting time, energy consumption, and tool wear. Insufficient allowance can leave portions of the casting surface uncleaned after machining, particularly when dimensional variation or distortion occurs.
| Design condition | Potential problem | Recommended action |
|---|---|---|
| Excessive stock on flat surfaces | Longer milling cycles | Optimize allowance according to casting capability |
| Excessive stock around bores | Longer boring operations | Review bore location and core design |
| Insufficient stock | Incomplete surface cleanup | Account for expected casting variation |
| Distorted critical features | Extra corrective machining | Improve geometry and solidification control |
Machining allowance should be established according to casting size, geometry, surface condition, production process, and required final accuracy. Large sand castings may need different allowances from smaller components.
For OEM projects, the design engineer, foundry, and machining supplier should agree on allowance values before production begins. Trial castings and historical inspection data can help establish practical values for each critical feature.
Material selection affects strength, wear resistance, cutting forces, and tool life. Gray iron and ductile iron are widely used in industrial manufacturing, but their graphite structures and mechanical properties differ.
| Material characteristic | Gray iron | Ductile iron |
|---|---|---|
| Graphite structure | Flake-shaped | Spheroidal |
| Main advantages | Good machinability and vibration damping | Higher ductility and toughness in suitable grades |
| Machining considerations | Generally favorable chip formation; hardness and carbides can affect tool wear | Cutting forces and tool life depend on matrix structure and hardness |
| Typical applications | Machine bases, engine blocks, equipment housings | Pump bodies, valve components, load-bearing parts |
Gray iron is often a practical choice for machine bases and housings where vibration damping and machinability are important. Ductile iron is frequently selected for components requiring greater tensile strength, ductility, or impact resistance.
The best material is not necessarily the one with the lowest machining cost. It must satisfy the component's strength, fatigue, wear, pressure, and service-life requirements.
Selecting an unnecessarily high-strength grade may increase material and processing expenses, while choosing a lower-strength grade that cannot meet the application requirements creates reliability risks.
For custom cast iron parts, discuss the required mechanical properties and machining conditions with the foundry before committing to a material grade.
A casting can be structurally sound but expensive to machine if it is difficult to locate, clamp, or reach with cutting tools.
Repeated repositioning increases setup time and creates opportunities for alignment errors. Deep, narrow pockets may also require long-reach tools, which can reduce cutting stability and increase tool wear.
To improve machining efficiency:
For example, if several mounting holes on a valve body can be drilled from one direction, the machining process may require fewer setups than a design that forces the operator to reposition the component several times.
For large industrial castings, stable workholding is particularly important because heavy weight and irregular geometry can increase handling time.
Each additional machining operation can involve setup, tool changes, inspection, and work-in-process handling. Even a short operation can add significant cost when repeated across a large production run.
During design reviews, check whether multiple operations can be consolidated or eliminated.
Useful opportunities include:
These changes can be particularly effective for medium- and high-volume production. For example, saving just two minutes per part across 5,000 components eliminates approximately 167 hours of machining time.
The calculation assumes the full two-minute reduction is achieved on every part. Actual savings depend on machine rates, production conditions, and the operations removed.
Good casting quality helps prevent expensive rework and rejected parts. Porosity, shrinkage cavities, inclusions, hard spots, and dimensional distortion can all affect machining efficiency.
A pore exposed during boring may make a pressure-containing pump housing unacceptable. Localized hard spots can accelerate tool wear or produce inconsistent cutting results.
Foundries can reduce these risks through appropriate gating and riser design, melt chemistry control, mold and core preparation, and solidification management. Dimensional checks before machining can also identify castings that are unsuitable for further processing.
Inspection requirements should reflect the component's application. Depending on the specification, quality control may include visual inspection, dimensional measurement, hardness testing, or appropriate nondestructive testing.
For critical custom industrial cast components, define acceptance criteria before production starts. Preventing defects at the casting stage is generally more economical than discovering them after substantial machining work has been completed.
The most effective cost reductions often come from reviewing the design before patterns, molds, and machining fixtures are finalized.
A foundry can identify difficult-to-cast features, recommend changes to wall thickness, and determine whether certain surfaces can remain unmachined. A machining supplier can evaluate tool access, datum selection, fixture design, and production cycle time.
A joint design review should address the following questions:
A casting that costs slightly more to produce may still be the more economical choice if it reduces machining time, scrap, and assembly problems.
When evaluating suppliers, buyers should consider the combined cost of raw castings, machining, inspection, rework, and rejected parts.
The following example illustrates how design optimization can change the total cost. These figures are hypothetical and are not industry-average prices.
| Cost per part | Original design | Optimized design |
|---|---|---|
| Raw casting | $45 | $47 |
| Machining | $30 | $19 |
| Inspection and rework allowance | $5 | $3 |
| Total manufacturing cost | $80 | $69 |
Although the optimized casting costs $2 more, total manufacturing cost falls by $11 per part, a reduction of approximately 13.8%.
At an annual volume of 5,000 parts, the potential saving reaches $55,000, provided the estimated costs and savings are achieved consistently.
This example highlights why sourcing decisions should be based on the complete manufacturing process rather than the quoted price of the raw casting alone.
Before releasing a cast iron component for production, confirm that:
Reducing machining costs requires more than relaxing tolerances or removing material. It means designing a component that can be cast consistently, machined efficiently, and inspected without unnecessary work.
By optimizing geometry, selecting suitable gray iron or ductile iron grades, controlling machining allowances, and simplifying workholding, manufacturers can reduce production time while maintaining the required quality and performance.
For OEMs sourcing custom iron castings, industrial sand castings, pump housings, valve bodies, and other heavy-duty components, early cooperation between the design team, foundry, and machining supplier is a practical way to control costs. A design that accounts for manufacturing requirements from the beginning can deliver more predictable production, fewer quality problems, and a lower total cost per part.


 IPv6 网络支持